


Minimum Order Requirement: $100 | Free Domestic Shipping on orders of $250 or more.
Elevator Buckets
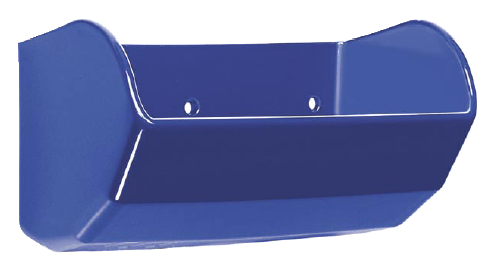
Elevator Buckets for Grain, Feed and Bulk Material Handling
Heavy-duty elevator buckets in polyethylene, nylon, and urethane for grain, feed, and bulk material handling — including FDA-compliant food-grade options from trusted makers like Tapco, Maxi-Lift, Nu-Hy, and 4B. Browse the full lineup below, or scroll down for sizes, styles, and applications.
We carry premium elevator bucket solutions for handling:
Grain • Feed • Fertilizer • Seed • Salt • Sand • Chemicals • Food products • Other free-flowing bulk materials
Our inventory includes standard and low-profile bucket styles for centrifugal discharge systems, along with FDA-compliant options for food-grade applications. Available in multiple sizes, colors, and capacities, these buckets are built for demanding environments where performance and reliability matter.
Whether you are replacing worn elevator buckets, upgrading a grain handling system, or sourcing components for a new conveyor setup, Jealco provides dependable products from trusted manufacturers such as Tapco and Maxi-lift.
New to bucket selection? See our Elevator Bucket Guide
Available Features
- Heavy-duty industrial construction
- Polyethylene, urethane, and nylon materials
- FDA-compliant bucket options
- High-speed centrifugal discharge designs
- Low-profile and super-capacity styles
- Corrosion-resistant materials
- Multiple bucket sizes and mounting configurations
Need matching hardware? Browse our selection of Elevator Bucket Fasteners to complete your installation.
Frequently Asked Questions
What are elevator buckets used for?
Elevator buckets are used in bucket elevator systems to vertically move bulk materials such as grain, fertilizer, feed, seed, sand, chemicals, and food products.
What material is best for elevator buckets?
Polyethylene elevator buckets are commonly used because they are lightweight, durable, corrosion resistant, and suitable for many agricultural and industrial applications. Nylon and urethane options are also available for specialized environments.
What is the difference between standard and low-profile elevator buckets?
Low-profile elevator buckets are designed for high-speed centrifugal discharge systems and can improve material handling efficiency while reducing product damage.
Are food-grade elevator buckets available?
Yes. Many elevator buckets are FDA compliant and suitable for food processing and food-grade bulk material handling applications.
Refine by
Filters
Filters
Powered by Lightspeed
Display prices in:USD
